
A sculpt becomes a print in four moves: make it one solid, give it clean topology, give it a real-world size, and export a format your slicer reads. Re:Form has a tool for each.
1. Make it one solid
Slicers want one continuous body, not loose floating parts.
- If the sculpt is several layers — body, horns, eyes — use Merge all in the Layers panel to combine every visible layer into a single mesh.
- Check for accidental leftovers first: hidden layers you forgot about, floating blobs. Split loose shows you what's actually disconnected — delete the debris, then merge.
2. Remesh into one continuous surface
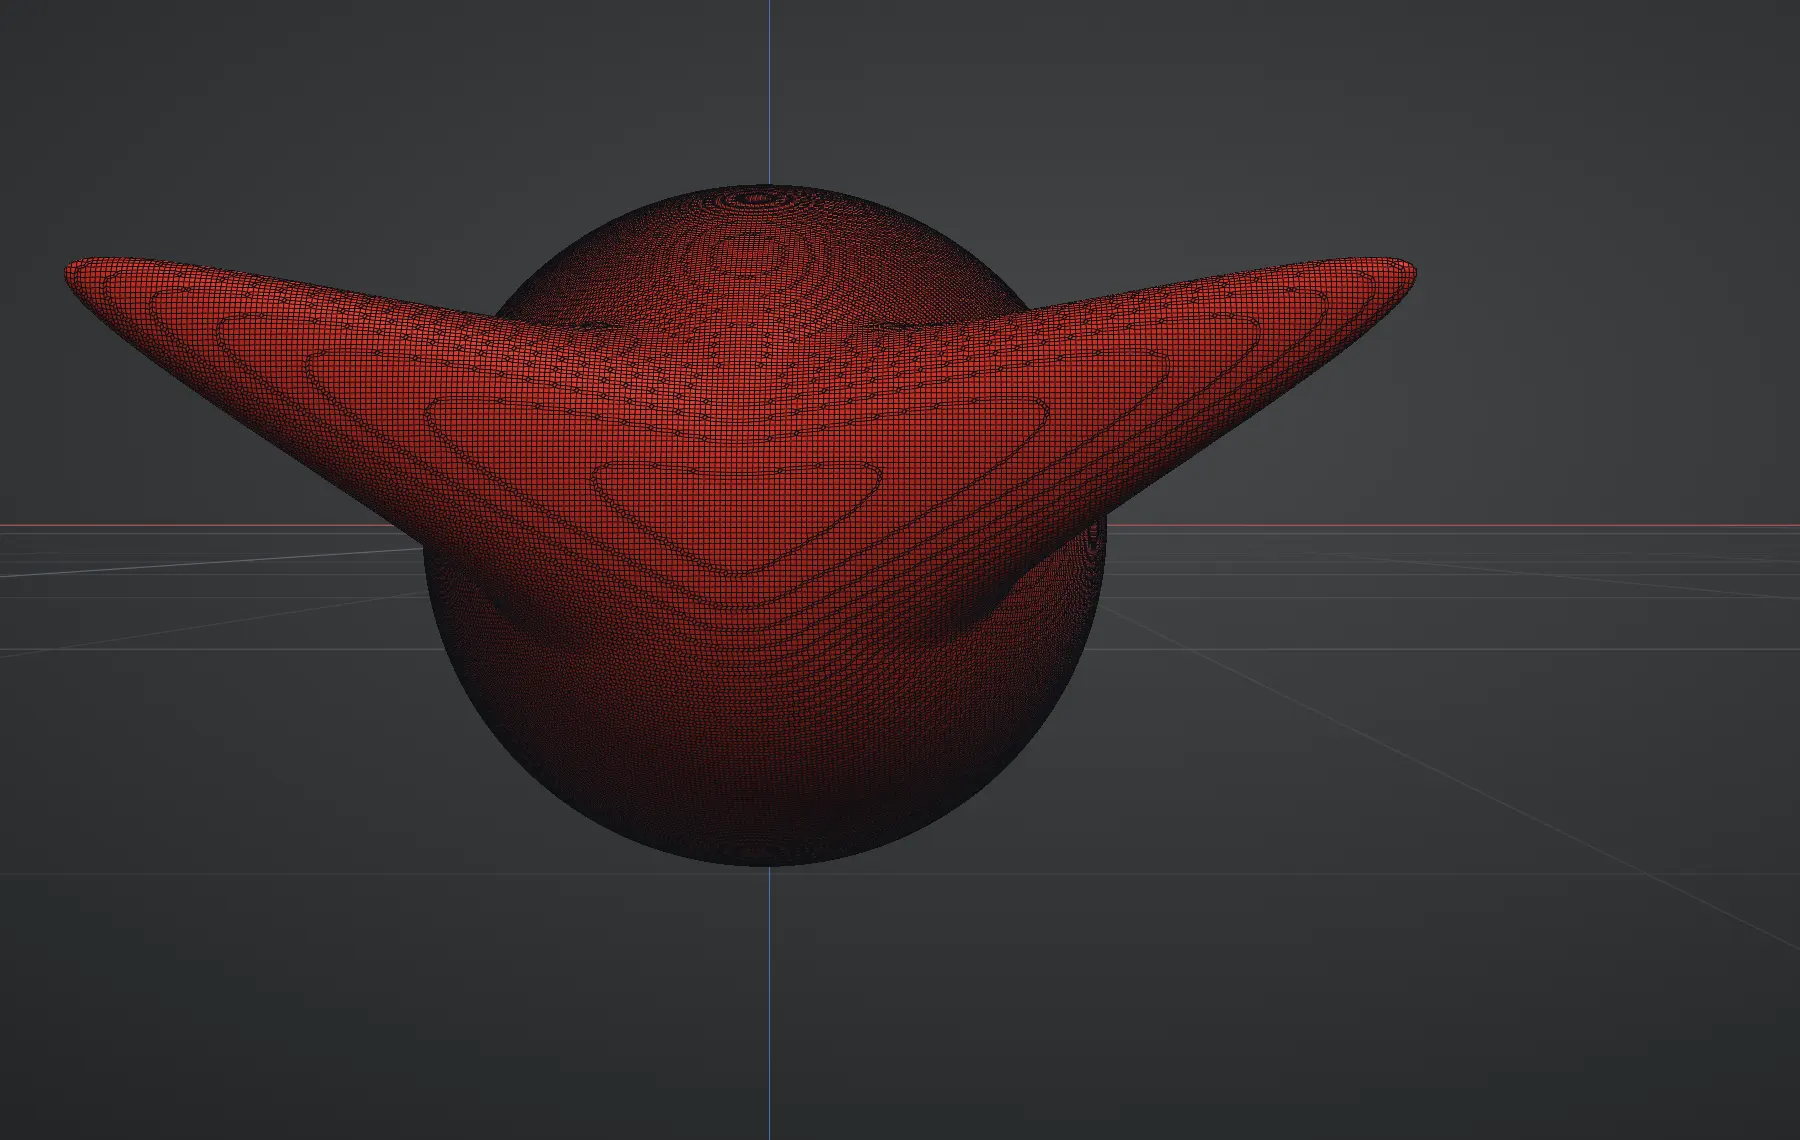
After merging, the parts still overlap rather than truly join. One press of Remesh rebuilds everything as a single continuous surface — intersections become real geometry, and the print becomes one object. Pick the Resolution to match your finest detail; 256 and up suits printable miniatures and busts.
3. Set the real-world size
In View ▸ Grid (or right-click Grid on the options bar), the Unit mm slider declares how many millimetres one world unit is — and every export scales by it, so your slicer reads true sizes instead of guessing.
Practical route: switch to Ortho (5), turn on the measurement grid, and read your sculpt's height in world units against it. If the sculpt stands 2 units tall and you want an 80 mm print, set Unit mm to 40. The line under the slider does the arithmetic with you (grid square size and export scale).
Before you export: Print check
Tools ▸ Print check… reads the active layer and tells you whether a slicer will accept it. It changes nothing; it is a report.
Print height, at the top of the window, is the height the model will be printed at, in millimetres. Walls and thin spots are worked out at that size. It is the same number as Unit mm said another way: typing a height sets Unit mm, so exports come out at that size too. Until a size has been set, 100 mm tall is assumed and the window says so.
- Closed says whether the surface is watertight. A slicer needs a closed surface to know inside from outside.
- Pieces counts the separate parts. Each one prints as its own solid, so floating debris shows up here. A closed part facing inwards inside another is counted as a cavity: the inner wall of a hollow model, which is how a hollow print should be.
- Size is the layer's width, depth and height in millimetres, at the Print height (the Unit mm you set in step 3). Volume appears when the layer is closed, which is what a resin or filament estimate needs.
- Triangles is the count your slicer will have to load.
- Open borders counts the openings and the open edges round them. Flipped faces counts triangles that face the wrong way, which slicers read as holes or as inside-out walls.
- Thin walls measures the model's thickness straight through from every point and counts the points thinner than Min wall, the slider under the report (1 mm to start; set it to what your printer and material can make). Walls under it break off or never print.
A line with a ⚠ is a problem. Two buttons help with them:
- Mask problem areas masks every point on an open border or a flipped face, so the trouble spots show up on the model. Orbit round, find them, and fix them with the brushes or a Remesh. One Ctrl+Z takes the mask back.
- The thin points are masked by Mask problem areas along with the rest: find them and thicken them with Inflate or Clay.
- Close holes is the same button as in the Topology section: it fills every opening no bigger than its Max hole size, and the check runs again by itself afterwards.
Press Check again after any change. When the last line reads Ready to print, export. The check looks at the active layer only, so Merge all first if the print is several layers. It does not judge overhangs; those are still yours and the slicer's to judge.
Hollow it, with drain holes
A solid print uses a lot of resin or filament and can warp as it cures. Tools ▸ Hollow… turns the active layer into a shell:
- Print height, at the top of the window, is the height the model will be printed at, in millimetres, as in Print check. Typing a height sets Unit mm; until a size has been set, 100 mm tall is assumed and the window says so.
- Wall is the thickness of the shell in millimetres, at that Print height (the window says the model's size in millimetres, so you can check that first). 2 mm suits most resin prints; 2 to 3 mm suits filament.
- Drain holes: 1 makes a hole at the bottom of the model, where it stands on the bed; 2 makes a second as far from the first as the bottom allows, so air can get in as the resin runs out; None seals the cavity, which most printers do not want. Hole size is the diameter; 3 to 4 mm drains well and is easy to plug.
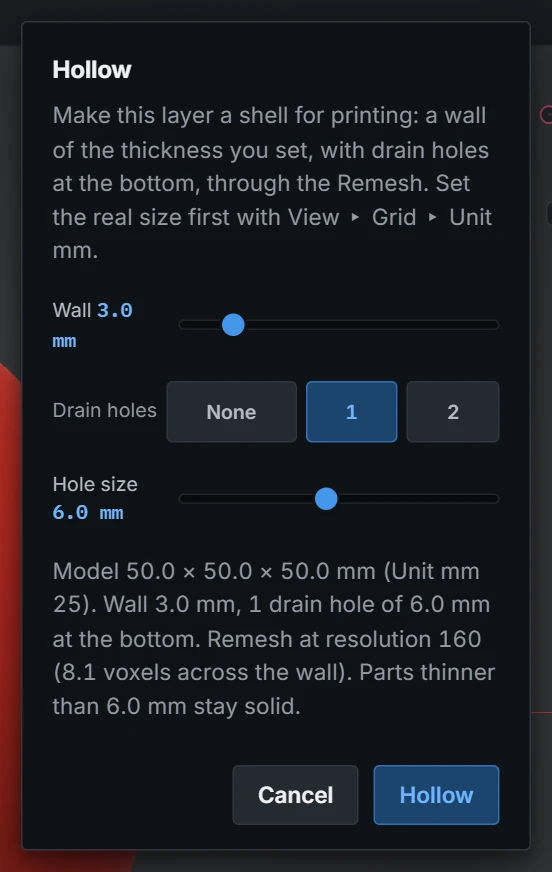
The window says what it will do and at what Remesh resolution: the grid is made fine enough for three voxels across the wall, so a thin wall on a large model means a finer, slower remesh. Press Hollow and the layer is rebuilt through the Remesh, like a Boolean, as one clean watertight piece: the outer surface, the inner wall, and the walls joined through the holes. Parts of the model thinner than two walls stay solid. Mask, paint and Mesh Sets do not survive the remesh, so hollow last. One Ctrl+Z brings the solid back.
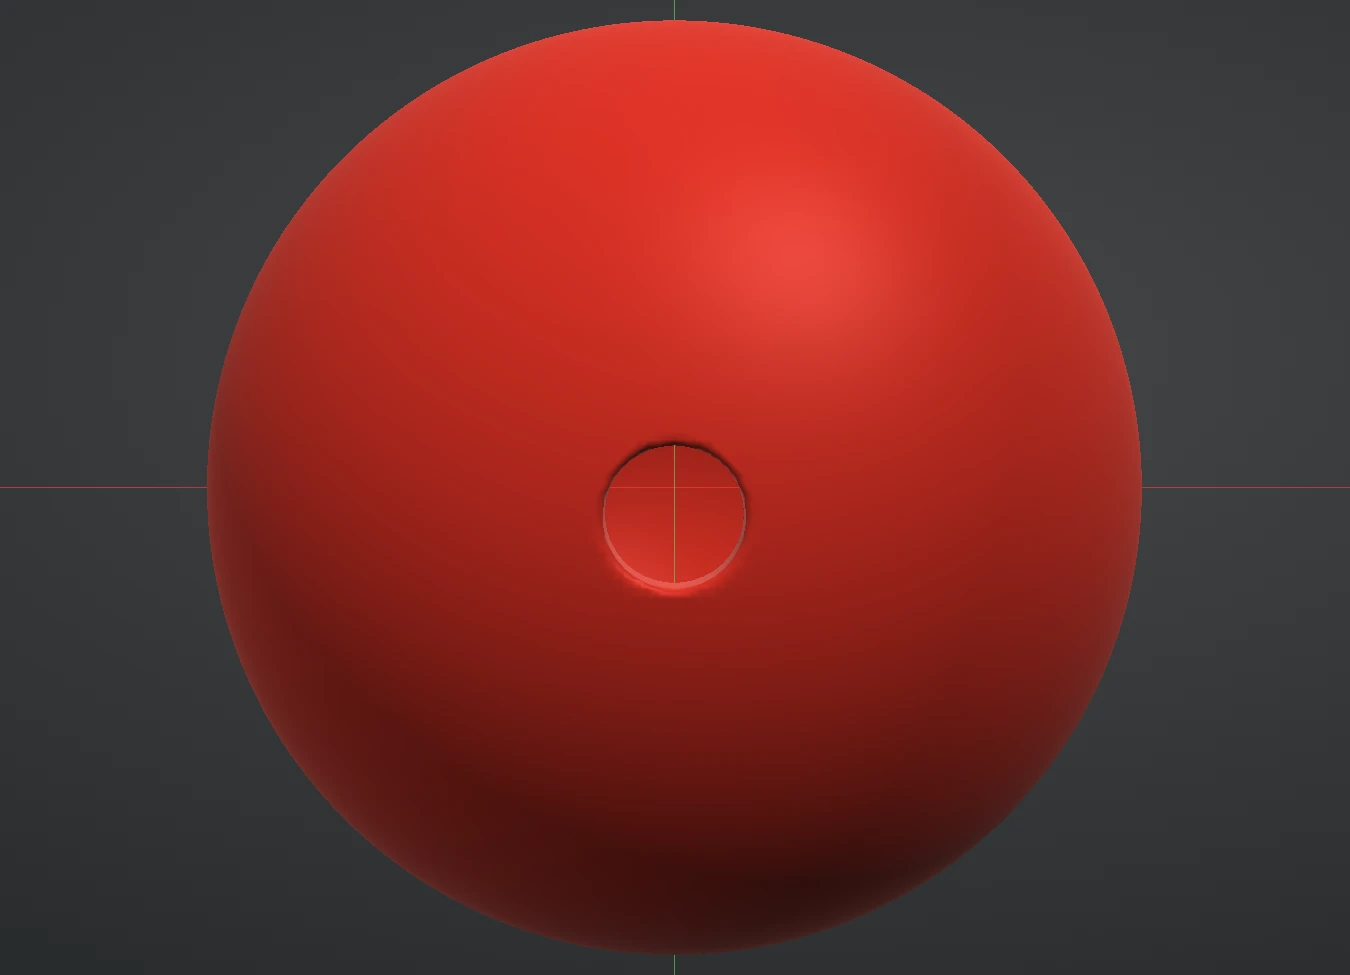
Run Print check afterwards: with a drain hole it reports one closed piece; with none it reports two pieces, one a cavity, which is right for a sealed shell.
4. Export
File ▸ Export ▸ STL is the slicer-native route (every plan); OBJ prints just as well — every slicer opens both. Drop the file into your slicer and the model arrives at the size you declared.
Design-for-printing notes
- Thickness: spindly fingers, whiskers and fabric edges that read on screen can be fragile below a couple of millimetres at print size. When in doubt, Inflate delicate parts a touch.
- Detail floor: printers have one. Detail much finer than your printer's resolution at the printed size costs triangles and gains nothing — sculpt for the size you'll print.
- Orientation and supports are the slicer's department; deep undercuts and long horizontal overhangs will earn supports, so consider them while posing.
Save the project before step 1 — the merged, remeshed print version flattens your layers, and you'll want the editable original the day a revision is needed.